AR
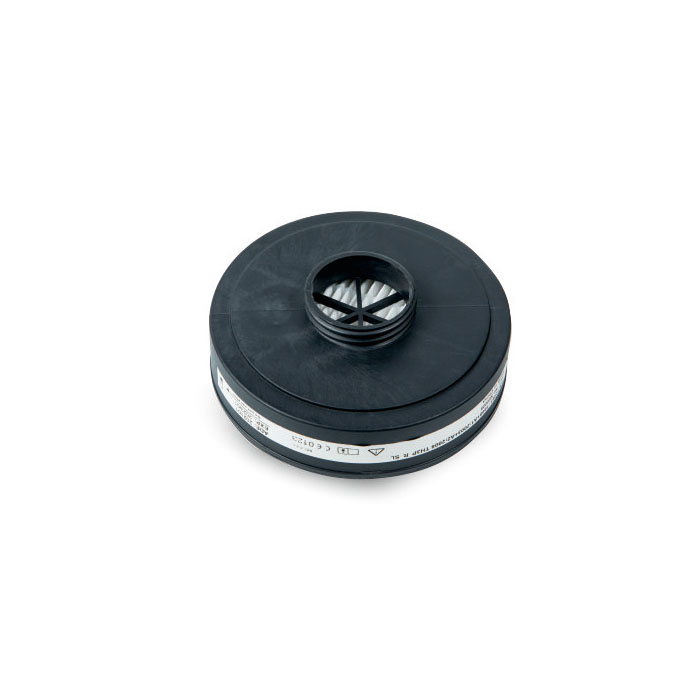
Celrith's ULPA grade dust filter box is a high-efficiency filtration component designed to remove PM0.3 particles at ≥99.999% efficiency while also adsorbing VOCs and odours. It is intended for use in clinical ventilator and anaesthesia circuits, industrial respirators, and high-specification air purification or oxygen generation equipment. By capturing fine particles and gaseous contaminants before they reach sensitive components, it helps protect both patients and equipment from harmful exposure.
In clinical and industrial settings, airborne contaminants are not just a comfort issue—they are a direct threat to equipment performance and user safety. Particles in the PM0.3 range can penetrate standard filters and accumulate inside ventilator circuits, anaesthesia machines, and respirator valves, leading to drift in sensors, increased resistance to airflow, and potential failure of critical components. Alongside particulate matter, volatile organic compounds (VOCs) and odours from disinfectants, anaesthetic gases, or industrial processes can be drawn into the air path, causing irritation or interfering with sensitive measurements.
Waterborne impurities are another concern in humidified breathing circuits or oxygen generation systems, where condensation can carry dissolved salts and biological matter into the filter media. Over time, these contaminants reduce filtration efficiency and shorten the service life of the filter box. The challenge is to capture both solid and gaseous contaminants without imposing excessive load on the system's fan or compressor.
When contaminants are not effectively removed, the consequences ripple through the entire system. In ventilators, particle build-up on flow sensors and valves can cause inaccurate tidal volume delivery, triggering alarms and requiring recalibration or replacement of expensive components. In industrial respirators, clogged filters increase breathing resistance, causing fatigue and reducing wearer compliance. For air purification and oxygen generation equipment, VOC breakthrough can saturate adsorbent beds prematurely, leading to frequent media replacement and downtime.
Moreover, the load on the system is not only physical but also economic. Higher filter change-out frequency, increased maintenance hours, and the risk of unscheduled downtime all contribute to higher total cost of ownership. Selecting a filter that balances high efficiency with low pressure drop is essential to relieve this load. The Celrith dust filter box is engineered to address these challenges by combining ULPA-grade particulate filtration with effective gas-phase adsorption in a single, customisable unit.
The Celrith dust filter box uses a composite media construction: a high-precision PTFE microporous membrane, advanced glass fibre, and activated carbon adsorption material. The PTFE membrane provides a physical barrier that captures particles down to PM0.3 with an efficiency of ≥99.999%, while the activated carbon layer adsorbs VOCs and odours. This dual-action design means one filter box addresses both particulate and gaseous contaminants, simplifying inventory and reducing the number of components in the breathing circuit.
The filter box is available in multiple ULPA grades, including U15 and higher, allowing you to match the filtration level to the specific requirements of your application. For equipment manufacturers, Celrith offers full customisation based on your drawings: we can mould the housing in medical-grade ABS or PC, and we use medical silicone gaskets with ultrasonic welding to ensure a leak-tight seal. This flexibility ensures that the filter box integrates seamlessly with your existing device design, whether you need a specific connector type, dimensions, or mounting configuration.
Every filter box is manufactured under GMP for medical devices, and our quality management system is certified to IATF 16949, ISO 9001, ISO 14001, and ISO 45001. Our CNAS-accredited laboratory validates filtration efficiency, pressure drop, and other performance parameters, so you can be confident in the consistency and reliability of each unit.
| Item | Detail |
|---|---|
| Product name | ULPA ventilator filter / respirator cartridge |
| Core filter media | High-precision PTFE microporous membrane / advanced glass fibre / composite activated carbon adsorption material |
| Particle removal efficiency | ≥99.999% for PM0.3 particles |
| Available grades | ULPA U15 and higher, multiple configurations |
| Main applications | Clinical ventilator and anaesthesia circuits, industrial respirators, high-specification air purification and oxygen generation equipment |
| Custom dimensions | Tooling and production according to customer drawings; medical-grade ABS/PC housing and medical silicone gasket with ultrasonic welding for leak-tight seal |
| Quality certifications | CNAS-accredited laboratory testing; GMP for medical devices; IATF 16949; ISO 14001; ISO 45001 |
The Celrith ULPA dust filter box is used across a range of critical applications. In clinical environments, it is a key component in ventilator and anaesthesia breathing circuits, where it protects patients from airborne pathogens and protects sensitive flow sensors from contamination. Industrial hygienists specify it for powered air-purifying respirators (PAPRs) and supplied-air systems where both particles and VOCs are present. Manufacturers of high-efficiency air purifiers and oxygen concentrators rely on it to meet stringent outlet cleanliness requirements.
Because the filter box can be customised to match specific device interfaces, it is also chosen by original equipment manufacturers (OEMs) who need a reliable filtration solution that integrates with their existing housing and pneumatic connections. Whether you are building respiratory therapy devices, industrial safety equipment, or specialty air handling systems, Celrith can tailor the filter media, housing, and connectors to your exact specifications.
Celrith operates a 50,000 m² manufacturing facility in Zhongshan, Guangdong, China, which includes six cleanrooms totalling 20,000 m².Our quality management system is certified to ISO 14001 and ISO 45001, and we comply with REACH and RoHS regulations, providing documentation to support your market access requirements. In 2024, we added IATF 16949 certification, further strengthening our ability to serve automotive and industrial customers.
Our CNAS-accredited laboratory enables us to validate filtration efficiency, pressure drop, and other performance characteristics, and we can issue test reports for each batch. With over 20 years of experience in filtration and more than 1,000 filtration solutions developed, we have the expertise to support your project from concept to production. Our automated production lines can deliver millions of filter units per month, ensuring reliable supply even for high-volume orders.
To receive a quotation or discuss a custom filtration solution, please provide the following details: your device or vehicle model, required dimensions or a drawing, airflow or water flow specifications, operating conditions (temperature, humidity, contaminant concentrations), and estimated quantity. Our engineering team will review your requirements and respond promptly. Contact us to start the conversation.
It removes PM0.3 particles with an efficiency of ≥99.999% and also adsorbs VOCs and odours through its activated carbon layer. This dual-action makes it suitable for both particulate and gaseous contaminants in ventilator circuits, respirators, and air purification systems.
The ULPA grade achieves ≥99.999% removal of PM0.3 particles. It is available in U15 and higher configurations. The filter box can be customised to fit most ventilator models based on your drawings or samples, ensuring compatibility.
Yes, Celrith offers full OEM/ODM customisation. We can mould the housing in medical-grade ABS or PC, adjust dimensions, and incorporate medical silicone gaskets with ultrasonic welding for a leak-tight seal. Simply provide your specifications or drawings.
Replacement frequency depends on the operating environment and contaminant load. For typical clinical use, we recommend replacing the filter box every 500 to 1,000 hours, or when pressure drop increases significantly. Regular monitoring ensures optimal performance.
The standard MOQ is 1,000 pieces, but it may vary by specification. Lead time for standard models is 7–15 days; custom orders typically take 25–35 days, excluding tooling time of about 15–20 days. We can prioritise large or seasonal orders to keep your supply chain stable.
Yes, we provide 1–3 free samples of standard specifications; you only cover the shipping cost. Custom samples may incur a fee, which is refundable upon bulk order. Samples are typically dispatched within 3–5 working days, with test reports included.
Celrith obtained GMP for medical devices in 2024. Our quality system is certified to ISO 9001, ISO 14001, ISO 45001, and IATF 16949. Our CNAS-accredited lab validates filtration efficiency, and we can supply compliance documents such as COA, COC, and MSDS.
Yes, we provide a complete compliance package, including test reports and material safety data sheets, to support your registrations in Europe, the US, Japan, and Korea. Our team is familiar with regional requirements and can assist with documentation.